

What Is Non Destructive NDT?
Non-destructive testing (NDT) encompasses a group of analysis techniques that evaluate the properties, integrity, and condition of a material or component without impairing its future usefulness. Where destructive testing requires the sacrifice of a specimen to obtain data, NDT generates information about defects, discontinuities, material properties, and dimensions while leaving the part fully intact and serviceable. This makes NDT the only practical approach for inspecting 100 percent of a production lot, verifying in-service components without removing them from operation, or assessing structures that cannot be replaced.
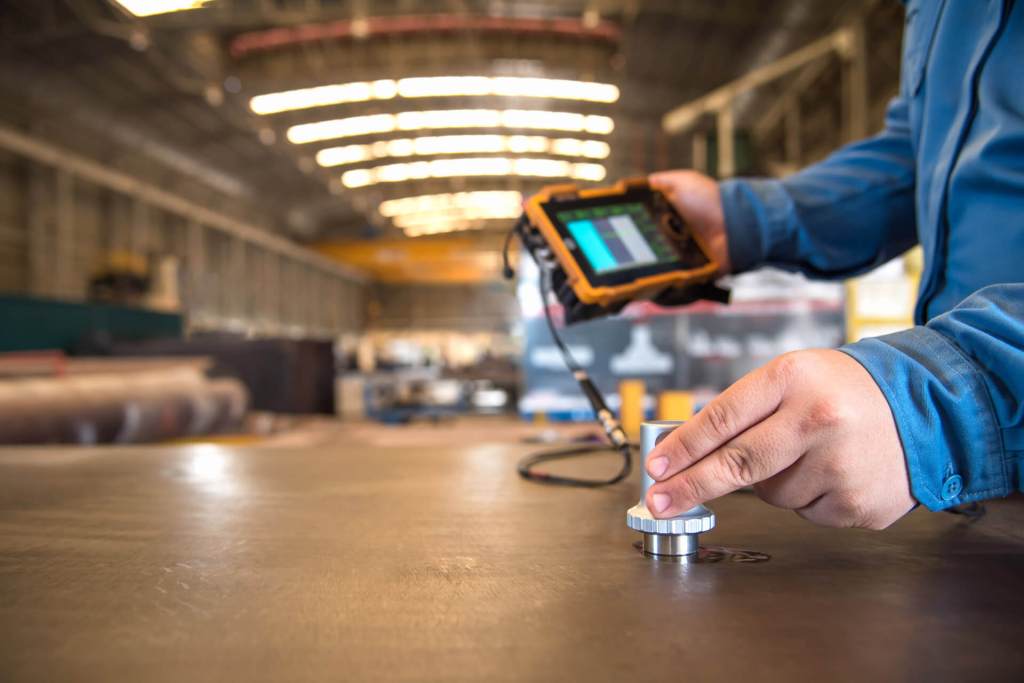
The major NDT methods each exploit a different physical principle to reveal internal or surface features. Ultrasonic testing (UT) uses high-frequency sound waves that reflect from internal discontinuities, measuring defect location by time-of-flight and characterizing defect size by reflection amplitude. Radiographic testing (RT) uses X-ray or gamma-ray transmission to project an image of internal density variations onto a detector or film. Magnetic particle testing (MT) reveals surface and near-surface cracks in ferromagnetic materials by detecting flux leakage at discontinuities when the part is magnetized. Liquid penetrant testing (PT) uses a capillary-action dye to detect surface-breaking defects. Eddy current testing (ET) uses induced electromagnetic fields to detect surface and subsurface defects in conductive materials, and phased array ultrasonic testing (PAUT) uses electronically steered ultrasonic beams to image complex geometries with greater coverage and speed than conventional UT.
NDT is applied across every industry where structural integrity, pressure containment, or safety-critical function depends on the absence of defects or the confirmation of material properties. Aerospace structures, pressure vessels, pipelines, nuclear components, turbine blades, welds, castings, and in-service bridges all require NDT as part of their manufacturing acceptance, periodic inspection, or maintenance programs. Method selection is governed by the material, geometry, defect type of concern, access constraints, and the applicable inspection standard.
Applications and Benefits of Non Destructive NDT Testing
Scope
NDT applies to metallic, polymeric, ceramic, and composite materials in virtually any product form – castings, forgings, welds, plates, tubes, and assembled structures. Each method addresses specific defect types and material classes. A complete NDT program typically combines two or more complementary methods to cover both surface and volumetric inspection requirements. Key evaluation areas include:
- Detection of internal voids, porosity, inclusions, and cracks (UT, RT, PAUT)
- Surface and near-surface crack detection in welds and high-stress areas (MT, PT, ET)
- Weld quality verification in fabricated structures and pressure vessels
- Wall thickness measurement of pipes, vessels, and corroded components
- Delamination and disbond detection in composite panels and bonded assemblies
- In-service inspection for fatigue crack growth in critical structural components
Applications
- Aerospace structural component manufacturing inspection and overhaul
- Pressure vessel and pipeline weld integrity verification
- Power generation turbine blade and rotor inspection
- Automotive casting and forging quality control
- Nuclear component inspection per regulatory requirements
- In-service bridge, crane, and structural steel inspection programs
Benefits
- Components remain fully serviceable after inspection – no material is consumed
- Enables 100 percent inspection of production lots without sampling compromise
- Detects defects before they reach critical size and cause failure
- Supports in-service inspection programs that extend component life safely
- Multiple complementary methods cover both surface and volumetric defect types
- Generates documented inspection records for regulatory, customer, and quality audit requirements
Non-Destructive Testing (NDT) Services Process
Method Selection and Procedure Development
The appropriate NDT method or combination of methods is selected based on material, geometry, defect type of concern
1Calibration and Setup
Equipment is calibrated using reference standards containing known artificial defects of the type and size specified in the acceptance
2Inspection Execution
The component is inspected per the written procedure. Coverage, sensitivity, and scanning parameters are verified during inspection.
3Evaluation and Reporting
Recorded indications are evaluated against the acceptance criteria defined in the applicable standard.
4Non-Destructive Testing (NDT) Services Technical Specifications
| Parameter | Details |
|---|---|
| Primary Methods | Ultrasonic (UT), radiographic (RT), magnetic particle (MT), liquid penetrant (PT), eddy current (ET), phased array UT (PAUT) |
| Applicable Standards | ASME, AWS, ASTM, ISO, MIL-SPEC, and customer-defined inspection procedures |
| Surface Methods | MT (ferromagnetic materials), PT (all materials, surface-breaking defects), ET (conductive materials) |
| Volumetric Methods | UT, PAUT, RT (internal defects at depth) |
| Personnel Qualification | ASNT SNT-TC-1A or NAS-410 Level II or Level III per method |
| Output | Inspection report with indication locations, characterization, and accept/reject determination |


- Ultrasonic flaw detector with A-scan, B-scan, and C-scan display capability
- Phased array ultrasonic instrument with encoded scanning hardware
- Digital radiography system or conventional X-ray film processing equipment
- Magnetic particle bench unit and portable yoke for field use
- Liquid penetrant materials (penetrant, developer, cleaner) per ASTM E165
- Eddy current instrument with surface and bobbin probe configurations
Equipment and Instrumentation Used for Testing
What You Receive: Test Report, Data, and Certification
- Inspection report with method, procedure reference, and equipment used
- Indication map showing location, orientation, and dimensions of recorded indications
- Accept/reject determination for each indication against specified acceptance criteria
- Calibration records for all equipment used during inspection
- Personnel qualification records for inspection personnel
- Quality assurance documentation
Non Destructive NDT FAQs
NDT can identify defects such as cracks, voids, corrosion, delamination, porosity, inclusions, and weld discontinuities without damaging the component. The detectable defects depend on the NDT method used.
The most suitable technique depends on the material, component geometry, expected defect type, and inspection objectives. Common methods include ultrasonic, radiographic, magnetic particle, liquid penetrant, and eddy current testing.
Yes. Methods such as ultrasonic testing (UT) and radiographic testing (RT) are capable of detecting internal defects that are not visible on the surface, making them ideal for evaluating structural integrity.
Yes. NDT is widely used for quality control during manufacturing as well as for inspecting components in service, helping identify defects without interrupting functionality or causing damage.
A nondestructive testing (NDT) laboratory inspects materials and components for defects without causing damage that makes them unusable. Technicians use methods such as ultrasonic testing, radiographic testing, magnetic particle testing, liquid penetrant testing, and visual inspection. The results help identify cracks, voids, corrosion, and other flaws while assessing component integrity.
An NDT facility provides specialized equipment, trained personnel, and controlled procedures to inspect materials, welds, and industrial components. Depending on the application, the facility selects appropriate testing methods, calibrates equipment, examines the component, and evaluates the results against relevant acceptance criteria. Findings are documented in a report to support quality assurance and safety.
An NDT testing lab examines components for internal and surface defects using suitable nondestructive techniques. The process involves sample identification, method selection, equipment calibration, inspection, and result interpretation. Techniques such as ultrasonic testing detect internal flaws, while dye penetrant testing reveals surface-breaking defects. The laboratory documents findings to help determine whether components meet applicable quality and inspection requirements.
Why Choose Infinita Lab for Non Destructive NDT Testing
When your Non Destructive NDT results have to hold up - for compliance, a customer audit, or an engineering decision - accuracy and an unbiased third-party report matter more than price. Infinita Lab routes your non destructive NDT testing to ISO/IEC 17025-accredited U.S. partner labs with hands-on method experience, so you get defensible data, transparent reporting, and turnaround times built around your project deadline - not ours.
Looking for an Accredited Partner for Non Destructive NDT Testing?
Send query us at hello@infinitalab.com or call us at (888) 878-3090 to learn more about our services and how we can support you.